Servo drives and frequency inverters are high-value core components for automated production. Improper operation and storage will cause premature hardware damage.
During operation: Keep good ventilation and heat dissipation for inverter cabinet. Avoid running under continuous over-load condition. Prevent conductive dust, oil mist from entering device interior. Regularly check cooling-fan working status; failed cooling fan is a common trigger for inverter over-temperature alarm.
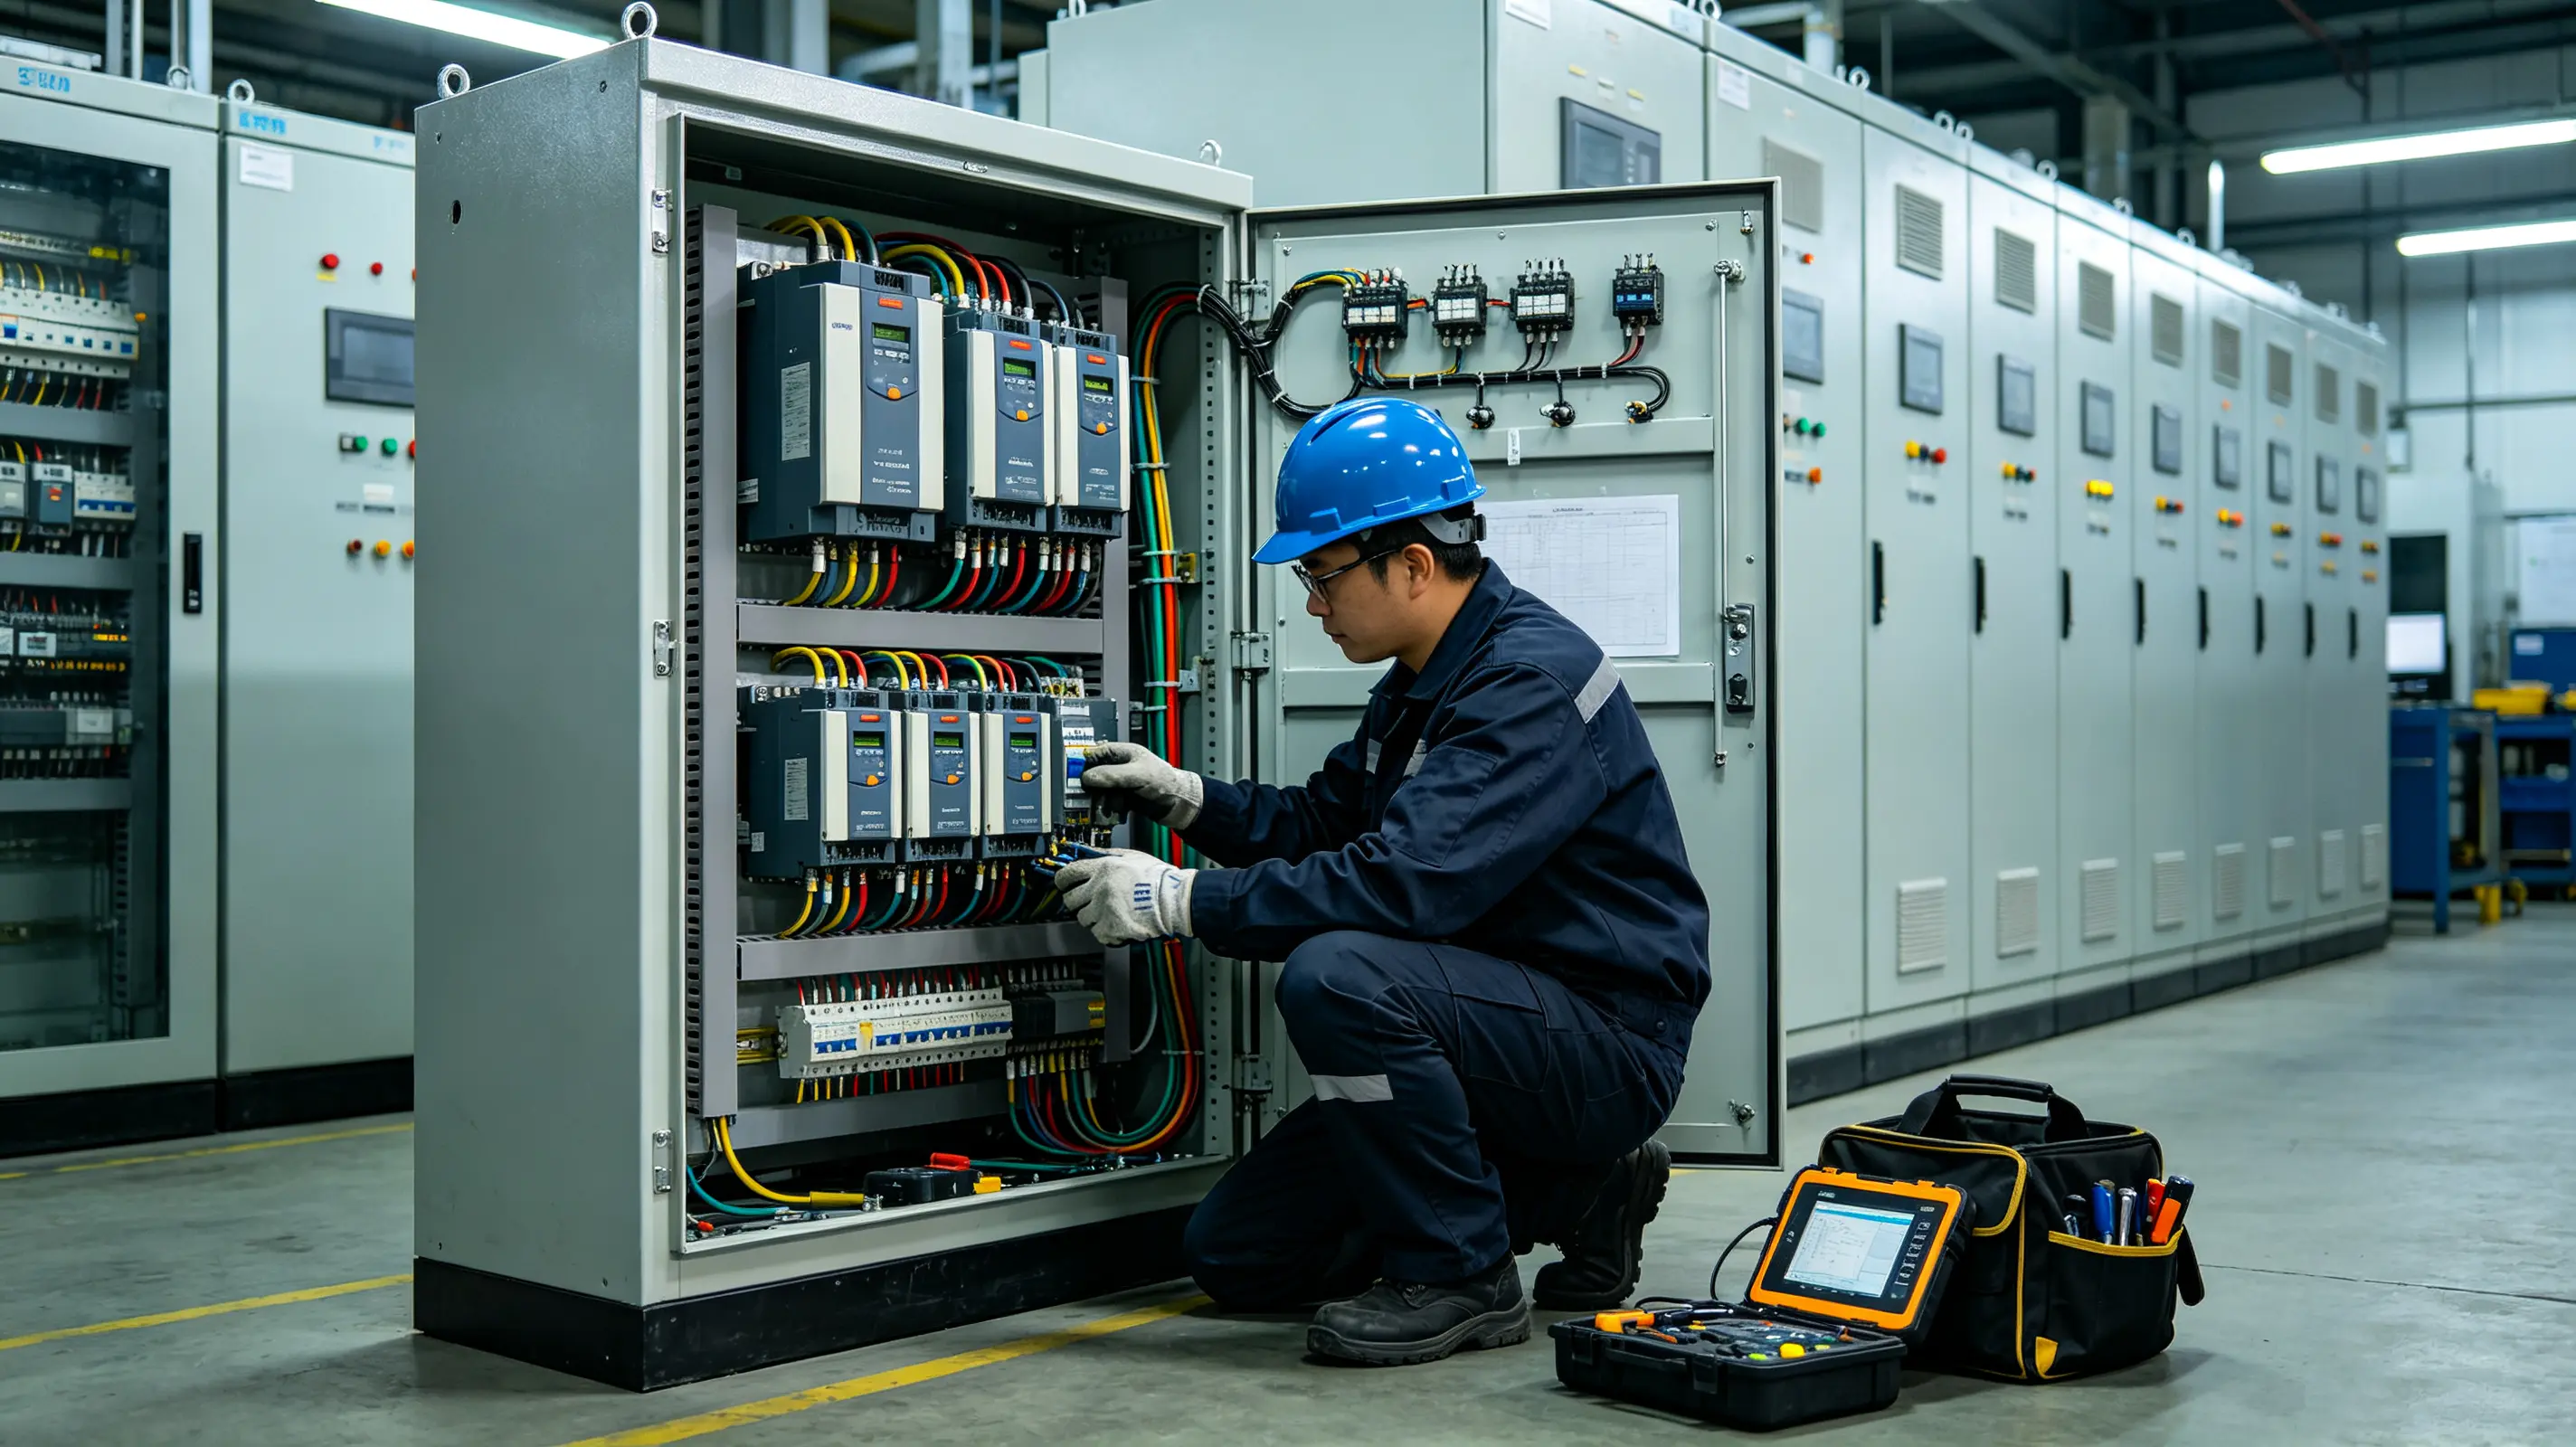
For standby spare-part inverters in warehouse: Do not store in damp or high-temperature environment. For long-term-stocked power-electronic products, perform periodic power-on test every 3-6 months to activate electrolytic capacitors, which can effectively lower capacitor-failure risk.
When drive unit breaks down, do not blindly replace internal components without professional testing. Wrong repair may expand fault scope and cause secondary damage.